Global Certifications That Build Trust
At Hongbang Packaging, quality is not just a promise; it is a standard we live by. To ensure that we consistently deliver the highest quality packaging solutions, we adhere to strict quality control systems, which are validated through various industry certifications. Our comprehensive approach to quality management guarantees that our products meet the highest standards of safety, functionality, and environmental sustainability.
We are proud to hold the following certifications:
ISO 9001: This globally recognized certification demonstrates our commitment to maintaining a quality management system that meets the rigorous demands of the international market.
ISO 14001: We are dedicated to minimizing the environmental impact of our manufacturing processes, and this certification validates our commitment to environmental sustainability.
ISO 22000: Ensures our packaging materials meet strict food safety management standards, guaranteeing safe, hygienic, and compliant solutions for global food packaging applications.
BSCI: Ensures our packaging materials meet strict food safety management standards, guaranteeing safe, hygienic, and compliant solutions for global food packaging applications.
BRC Packaging Certification: This certification further ensures that our products are safe, legal, and of high quality, making us a trusted supplier for food and consumer goods packaging.
FDA Compliance: We ensure that our packaging products used in food and beverage industries meet all required regulatory standards, including compliance with the U.S. Food and Drug Administration (FDA) regulations for food-safe packaging.
SGS Testing: As part of our commitment to product excellence, we regularly undergo third-party testing by SGS to ensure that our packaging materials meet international safety and performance standards.
Through these certifications and ongoing quality assurance processes, Hongbang Packaging continues to deliver products that not only meet but exceed customer expectations.
Approved by ISO9001, ISO14001, ISO22000, ISO13485, BSCI, BRC, FDA etc.

ISO 9001

ISO 14001

ISO 22000

bSCI

BRC

CFR

FDA

EPR

Medical

Other
Why Certification Matters in Flexible Packaging
In today's competitive packaging industry, certified manufacturing is essential for ensuring product safety, regulatory compliance, and brand credibility. Buyers are no longer selecting suppliers based solely on price; they require partners who can demonstrate traceability, consistency, and risk control.
Certified packaging provides safer food and pharmaceutical packaging solutions, reduces regulatory risks for import and export, enhances brand trust and market competitiveness, and ensures stable and repeatable production quality.
As one of the top 10 flexible packaging manufacturers in China, HongBang Packaging integrates certification requirements into every operational detail, making compliance a natural outcome of our daily processes.
Wide Applications of Flexible Packaging Products
Our packaging solutions are widely applied across multiple industries, delivering both protection and strong visual appeal.
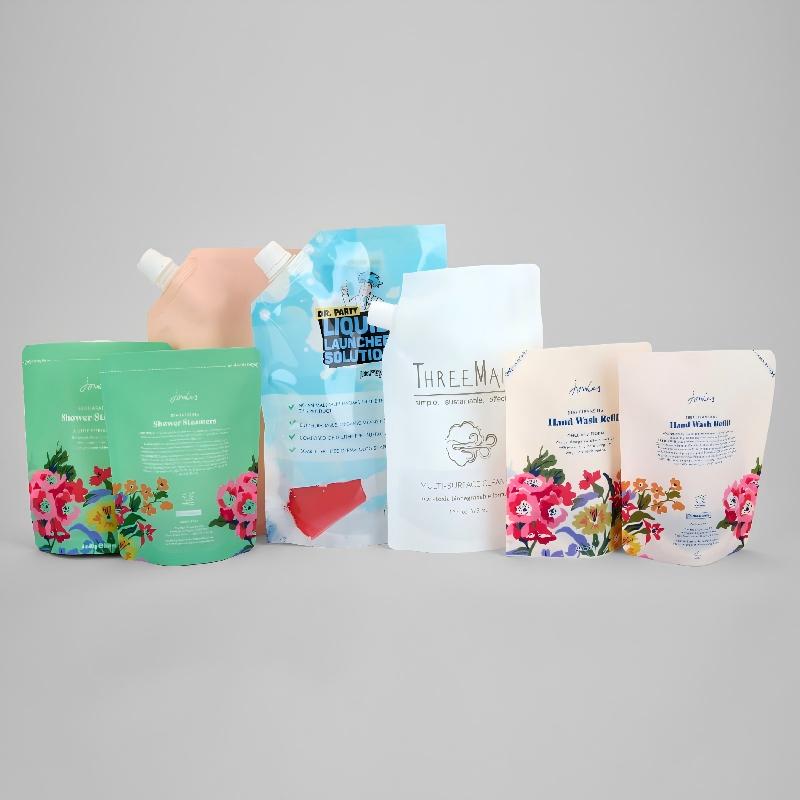
In the food and beverage sector, we provide coffee packaging with one-way degassing valves, snack and dried food packaging with high barrier protection, vacuum bags for frozen and fresh food preservation, and spout pouches for beverages and liquid foods.
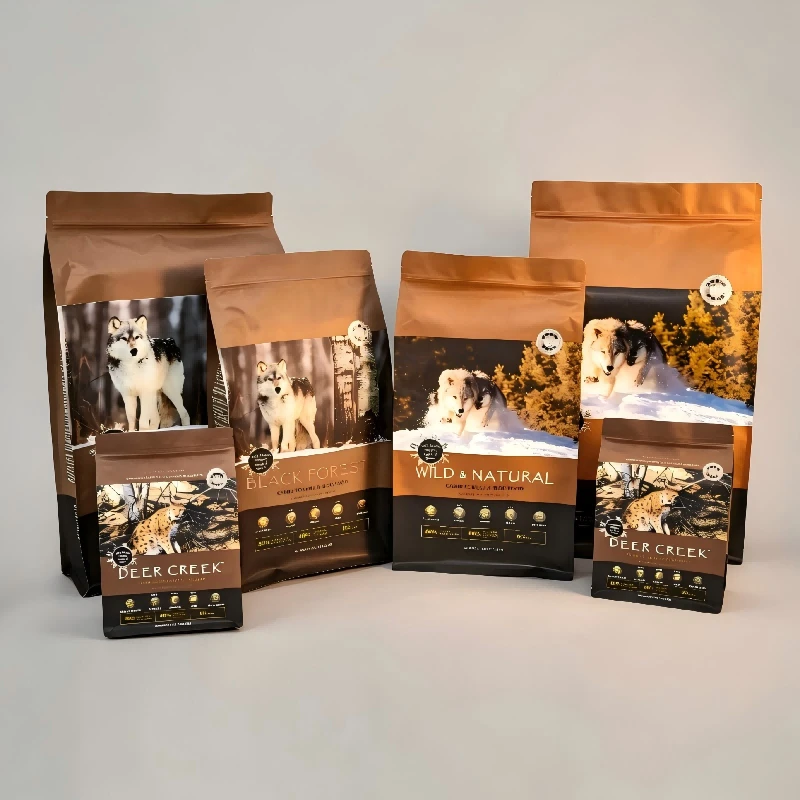
In the pet food industry, we offer durable and puncture-resistant packaging for dog and cat food, moisture-proof structures to maintain freshness, and premium printing to enhance brand positioning.
For pharmaceutical and healthcare applications, we produce medical-grade packaging compliant with ISO13485, high-barrier structures for sensitive products, and secure sealing solutions for contamination prevention.
We also support specialty products such as herbal medicine, nutraceuticals, child-resistant packaging, irregular-shaped bags, and high-end customized packaging for premium markets.


Food Packaging
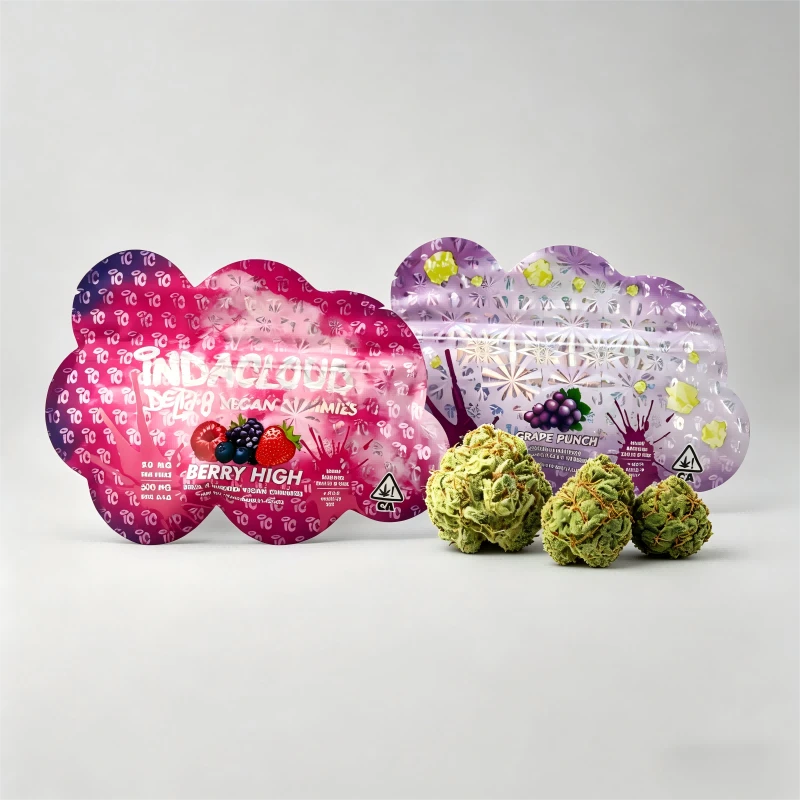
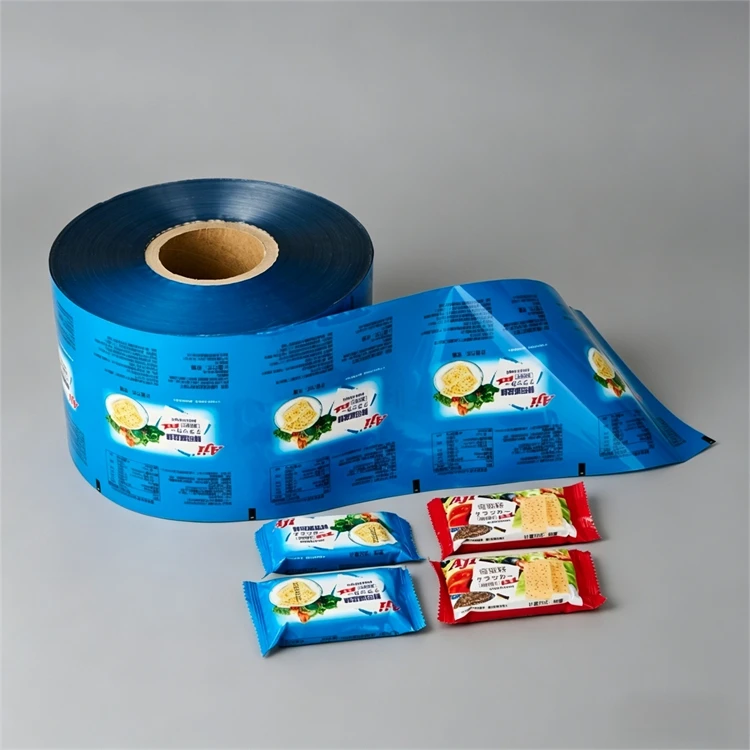
Food packaging is our core application area. Our certified food-grade packaging is ideal for snacks, baked goods, confectionery, frozen food, seasonings, grains, dried fruits, and other food products. PP materials deliver excellent heat resistance for microwaveable packaging; PET provides high transparency and glossy appearance to enhance product display effects; PE offers superior flexibility and moisture-proof performance. High-barrier composite packaging effectively blocks oxygen, moisture, and odor, greatly extending the shelf life of food. All food packaging fully complies with FDA, ISO22000, and BRC standards, ensuring safe direct food contact.
Pet Food & Supplies Packaging
We provide durable, odor-proof, and high-barrier packaging solutions for pet food, cat litter, pet treats, and pet care products. The strong sealing and anti-oxidation properties keep pet food fresh and palatable, while customized premium printing helps pet brands improve product recognition and market appeal.
Beverage & Daily Necessities Packaging
For beverages, personal care, cleaning products, cosmetics, and household items, our packaging features excellent leak-proof performance and stable color printing. We use high-strength materials to ensure product safety during transportation and storage, while fashionable design and exquisite craftsmanship enhance brand image.
Medical & Health Product Packaging
Supported by ISO13485 certification, we produce hygienic, sterile, and stable packaging for medical supplies, sanitary products, and health care items. The materials are non-toxic, odorless, and feature excellent isolation performance to protect medical products from contamination, moisture, and damage.
Industrial & Electronic Product Packaging
We also design anti-static, moisture-proof, and shock-resistant packaging for industrial parts, electronic components, hardware, and tools. The packaging effectively protects products from collision, dust, and humidity, meeting the requirements of long-distance logistics and long-term storage.
Eco-Friendly & Sustainable Packaging
Responding to global low-carbon and environmental trends, we actively develop biodegradable packaging, recyclable materials, and lightweight packaging solutions. Compliant with EU environmental directives and global green standards, our eco-friendly packaging helps brands fulfill their low-carbon social responsibilities and meet increasingly strict environmental regulations.
Advanced Custom Packaging Solutions
We provide fully customized packaging solutions tailored to your product and market requirements.
Our customization capabilities include multiple bag types such as Stand-up Pouches, Flat Bottom Bags, zipper bags, spout pouches, and packaging roll films. We offer flexible material structures including PE, PP, PET, and aluminum foil combinations. Printing options include high-definition gravure printing and low-MOQ digital printing. Functional features such as valves, zippers, tear notches, and child-resistant closures are also available.
From a technical perspective, our packaging solutions provide high barrier protection against oxygen, moisture, and UV light, as well as anti-fog and anti-static properties. We also offer high-temperature resistant materials suitable for retort applications and environmentally friendly options such as recyclable packaging.
Our R&D team ensures every solution balances performance, cost efficiency, and visual impact, helping products stand out in competitive markets.